Every batch, tested and traceable.
Raw materials, in-process samples and finished products are tested against pharmacopoeial specifications before anything leaves our plant.
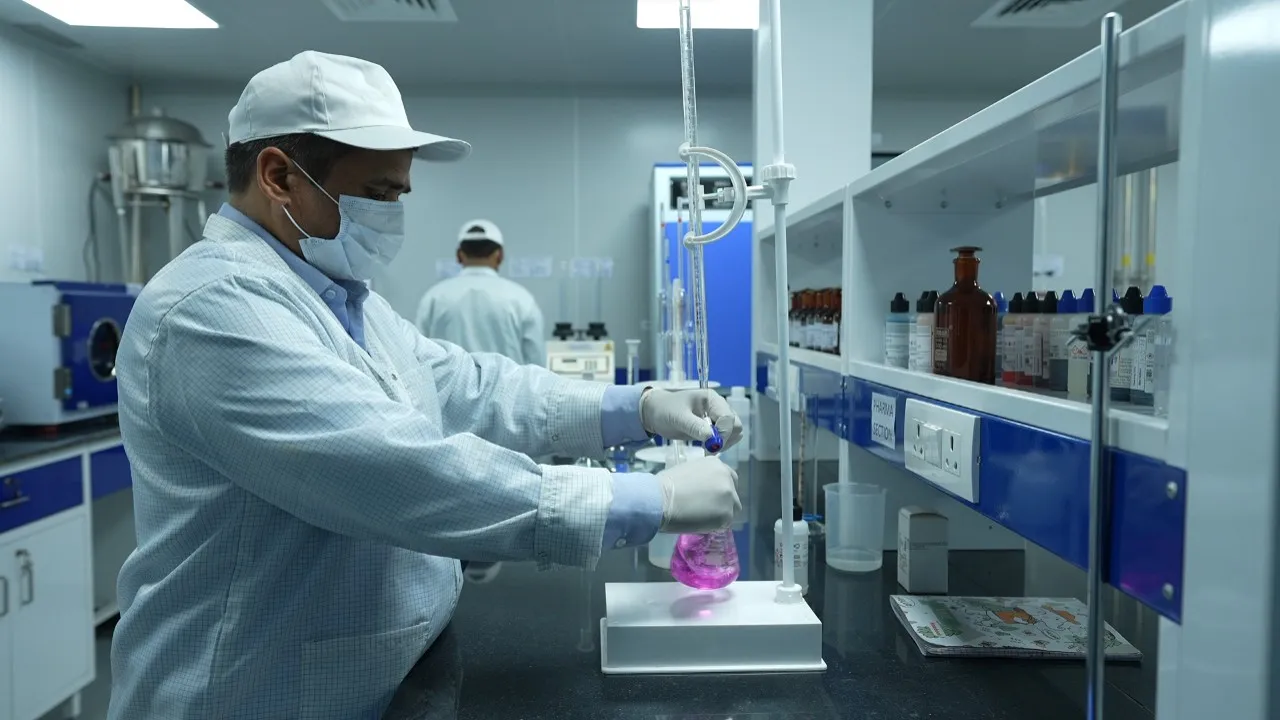
Five layers of assurance.
Analytical laboratory
HPLC, GC, UV-visible spectrophotometers, dissolution testers, titrators, precision balances and particle size analysis.
Microbiology laboratory
A separate micro lab for microbial limits of raw materials and products, and monitoring of the manufacturing environment.
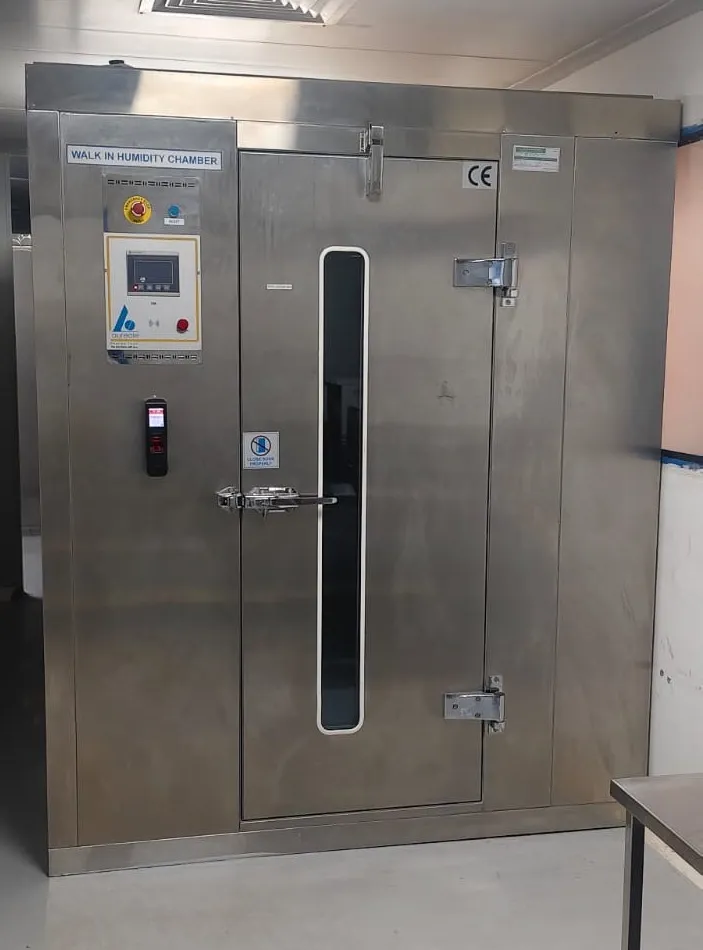
Walk-in stability chamber
Controlled temperature and humidity for long-term and accelerated stability studies of our products.
Quality management system
Document control, change control, deviations and CAPA, equipment calibration, and training records, run to GLP.
Digital operations
Electronic batch records, a digital QMS and QC workflows on our in-house software platform, for end-to-end traceability.
Walk-in stability chamber.
Controlled temperature and humidity for long-term and accelerated stability studies, so every shelf life we print is backed by data.
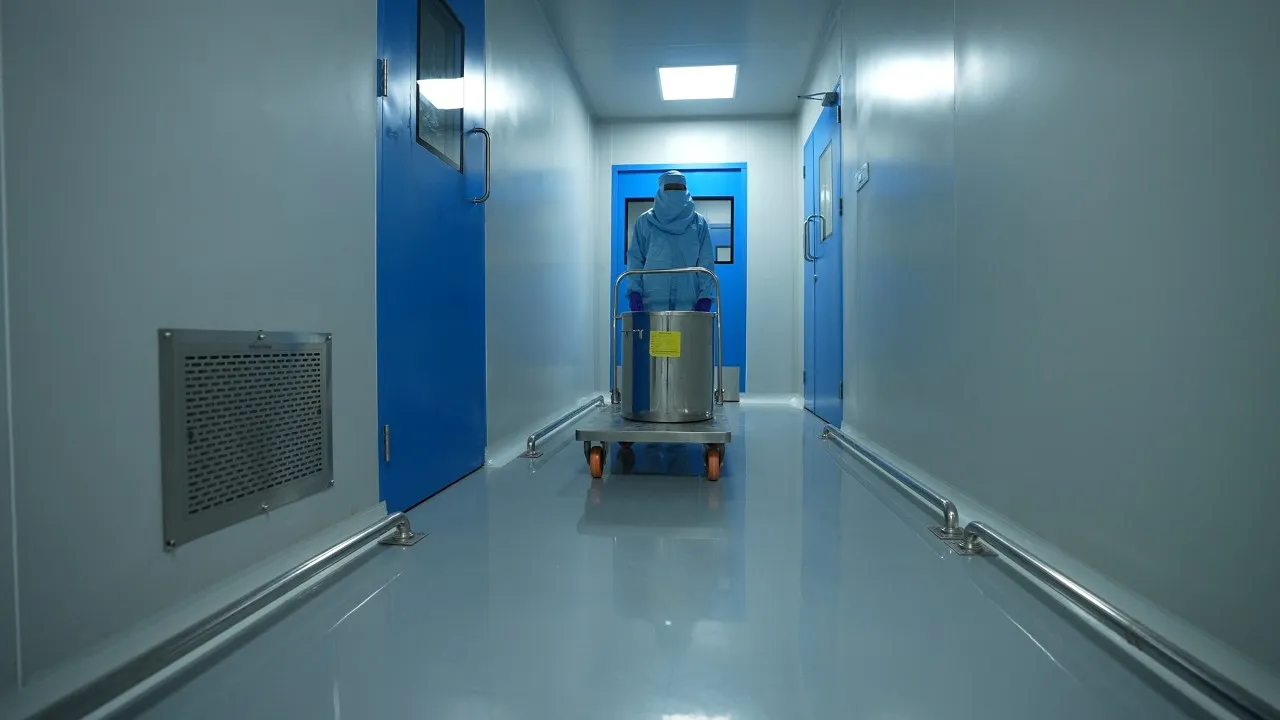
Designed so products never meet.
- Separate personnel and material flow through airlocks into every suite
- One AHU per area, 40 in total, holding pressure, temperature and humidity
- Segregated production areas for each product category
- RO-EDI purified water below 1 µS/cm conductivity
Report a quality concern.
Every complaint is logged, investigated and answered by our QA team.