Production unit · since 2023

Built for clean, consistent production.

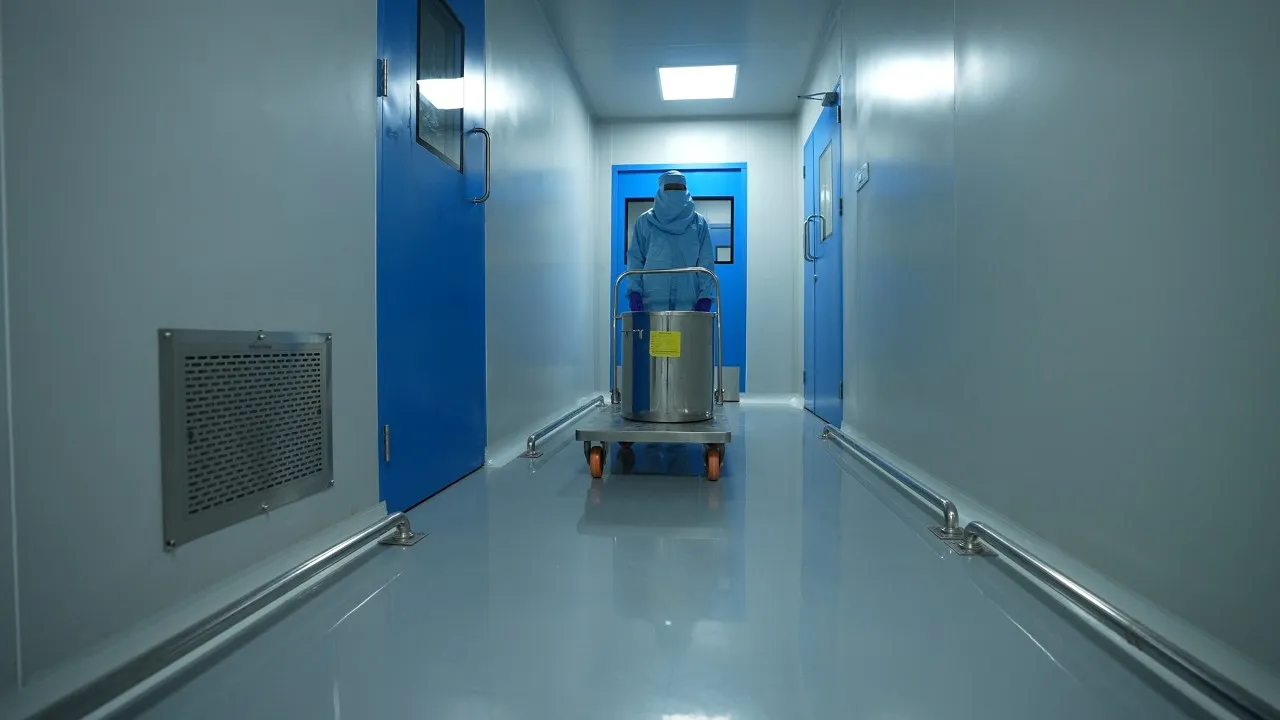
90,000 sq ft designed to cGMP, with separate personnel and material flow and a dedicated AHU for every area.

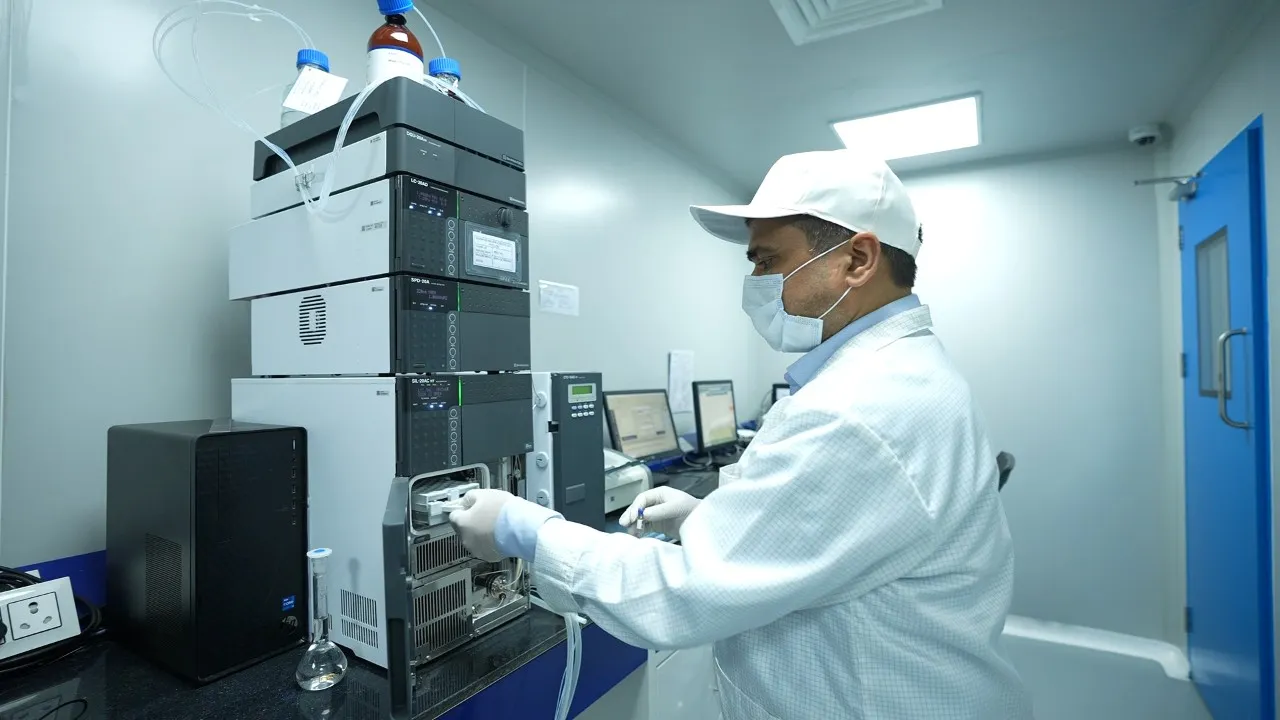
Cleanroom corridorsTablet compressionCapsule fillingExternals manufacturingBlister packingQuality control laboratory
Tablets a year
3.6B
Capsules a year
720M
Externals a year
60M
Oral solid dosage · general section

Tablets and capsules.

Follow a batch from the store to the blister pack.

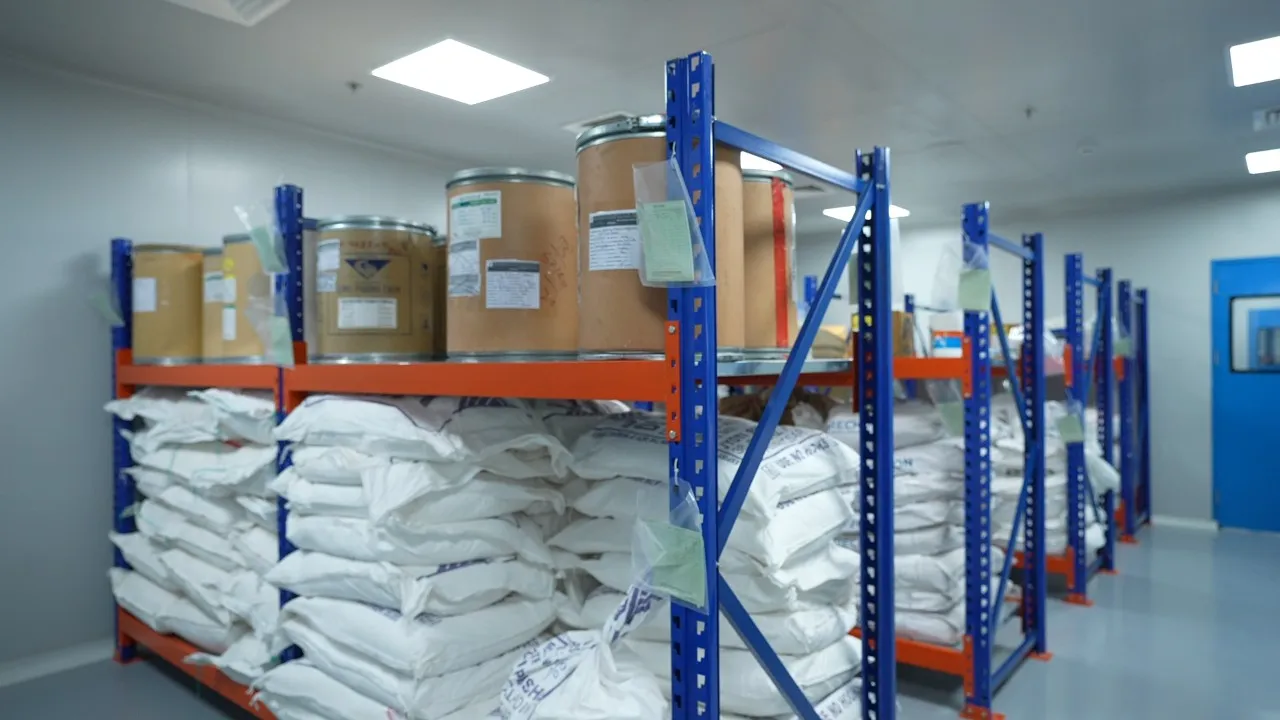
Raw material store
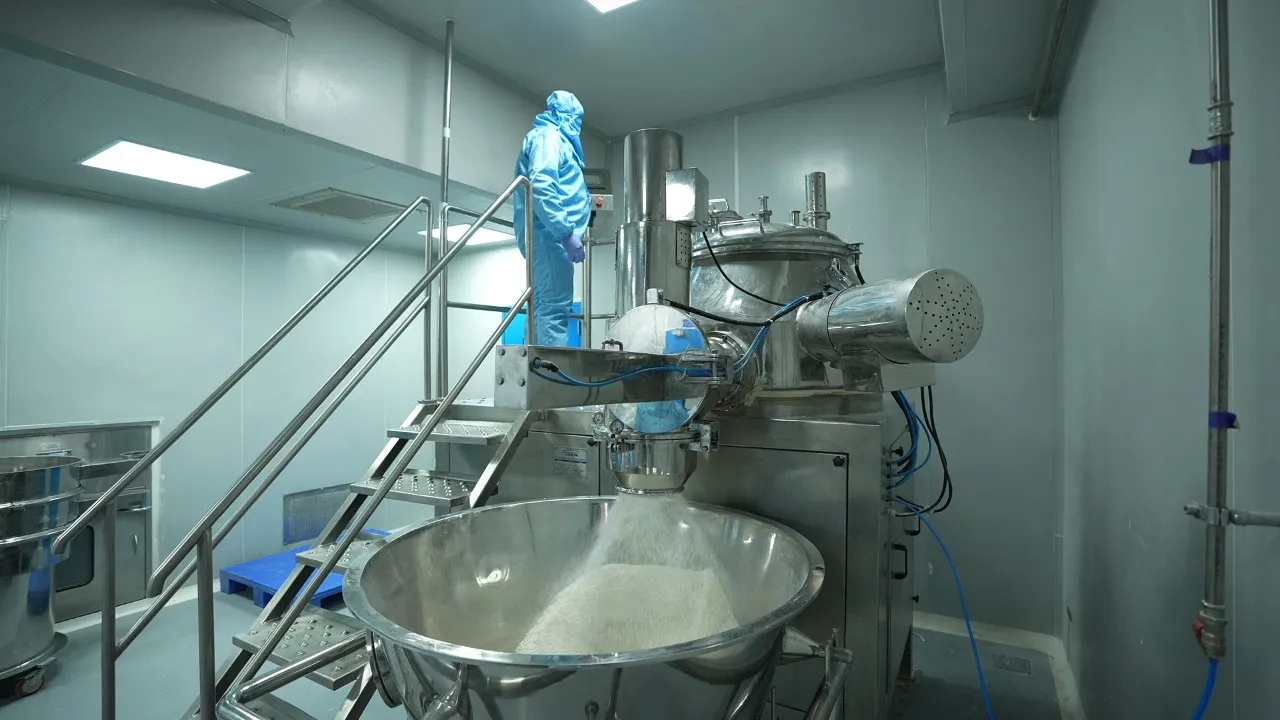
Blender
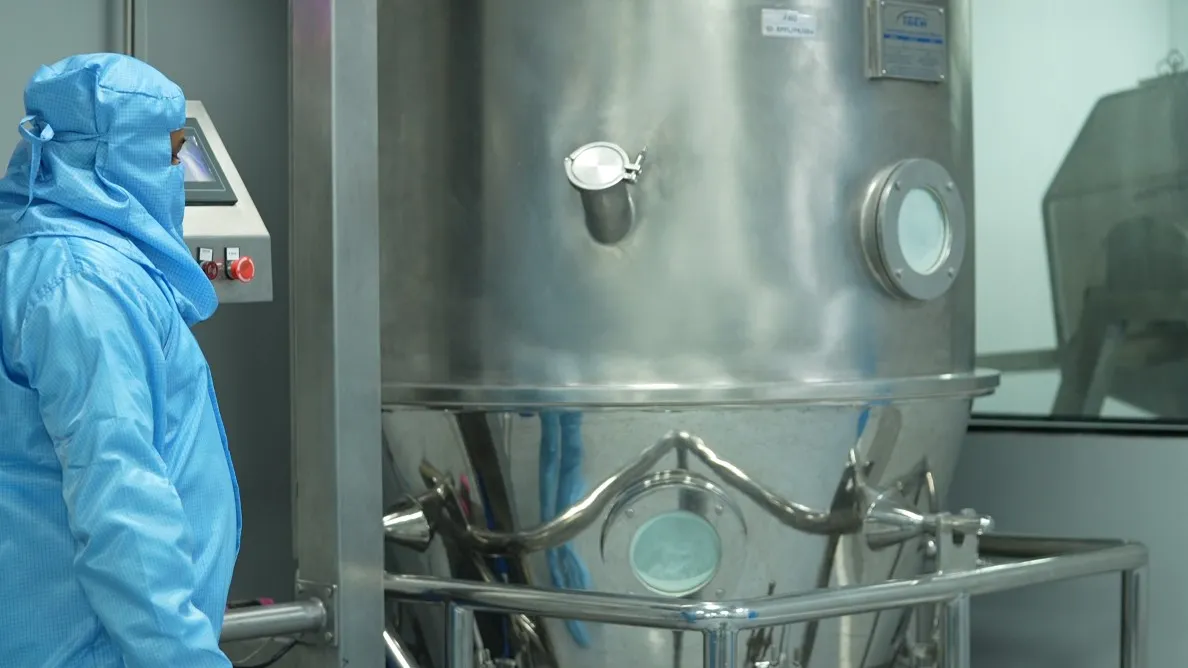
Fluid bed dryer
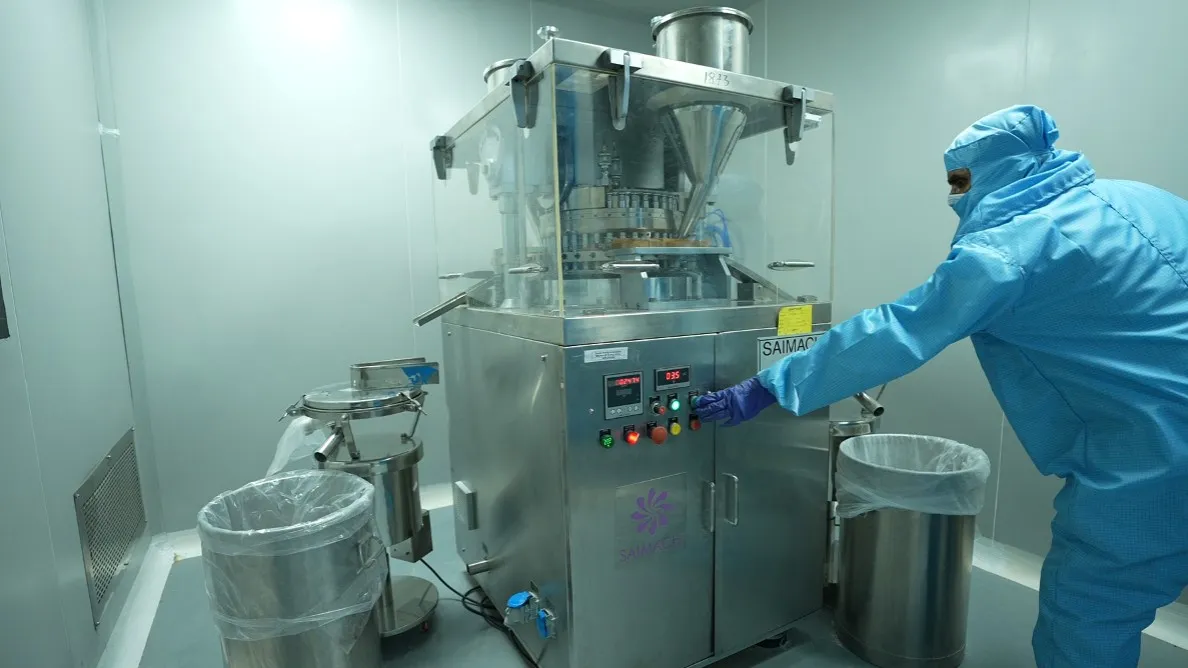
Rotary tablet press
Auto-coater
Capsule filling machine
Blister packing line
01 · Stores

It starts in the store.

Raw materials are received, quarantined, sampled and released by QC before they reach production.

02 · Blending

Weighed and blended.

Dispensing under controlled conditions, then blending to a uniform mix in dedicated suites.

03 · Granulation and drying

Granulated. Dried. Consistent.

Fluid-bed drying brings every granule to the same moisture, so compression behaves the same every time.

04 · Compression

3.6 billion tablets a year.

Rotary presses in segregated cubicles, each area served by its own air handling unit.

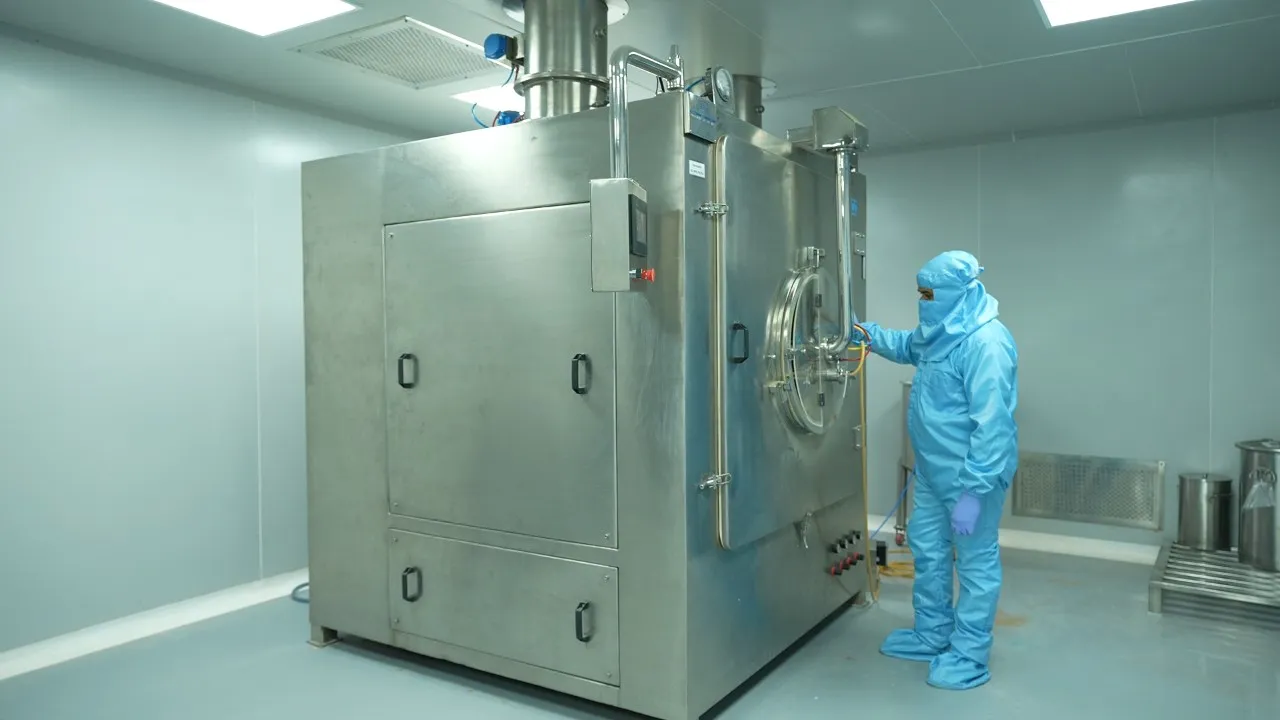
05 · Coating

Film-coated and sustained-release.

Automatic coaters apply film coats for taste, stability and controlled release.

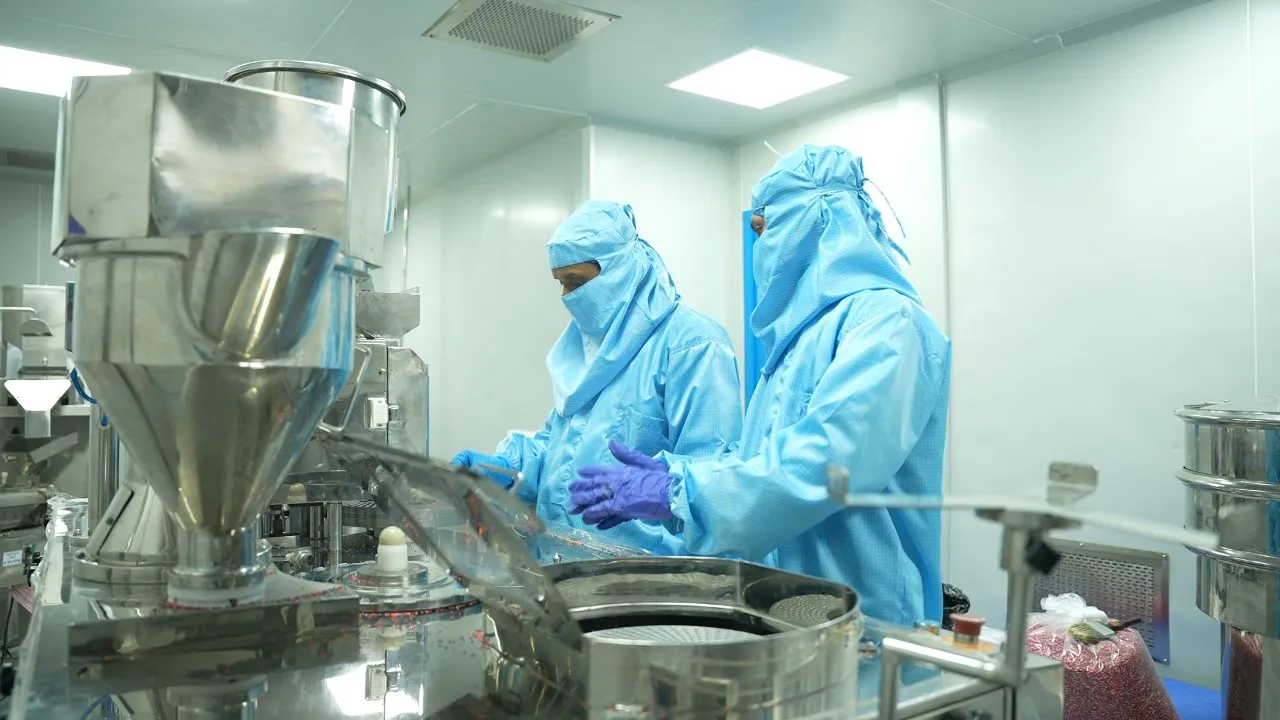
06 · Capsules

720 million capsules a year.

Automatic hard gelatin capsule filling with in-process weight checks.

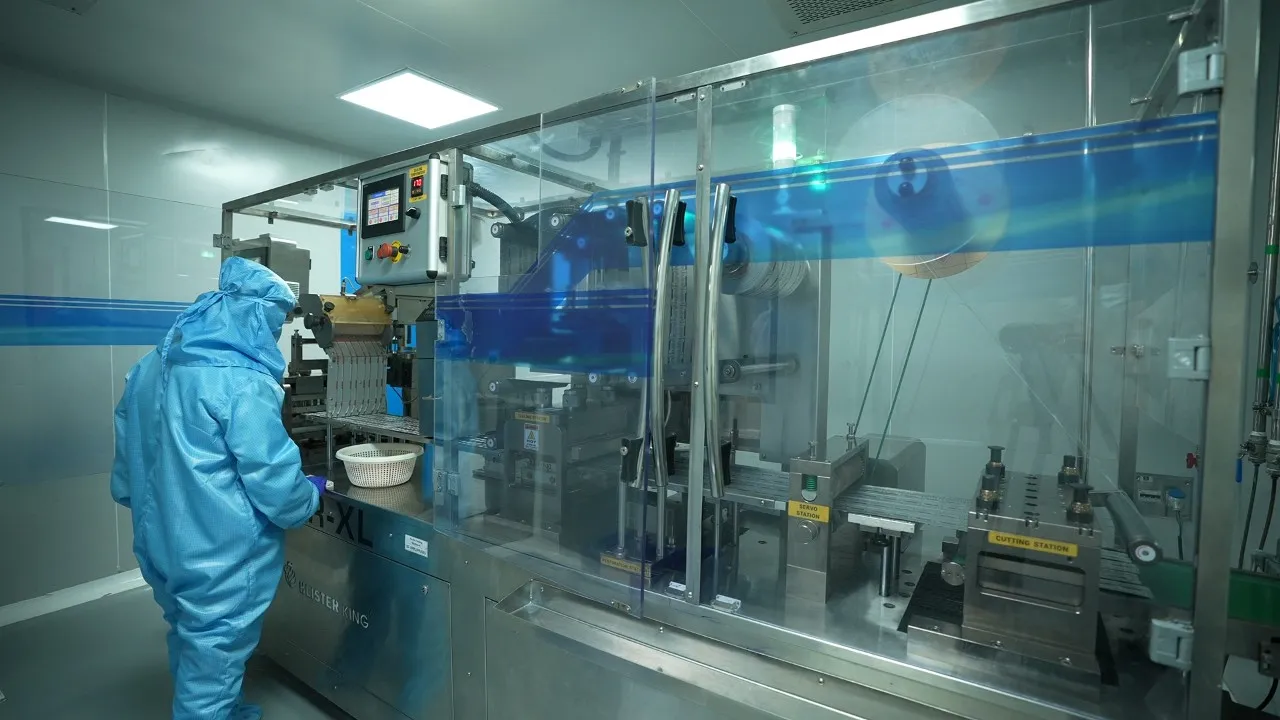
07 · Packing

Packed for India and the world.

Blister packing lines finish the product for domestic brands, partners and export markets.
Externals · general section

Topicals, made apart.

Ointments, creams, gels and lotions in their own block.

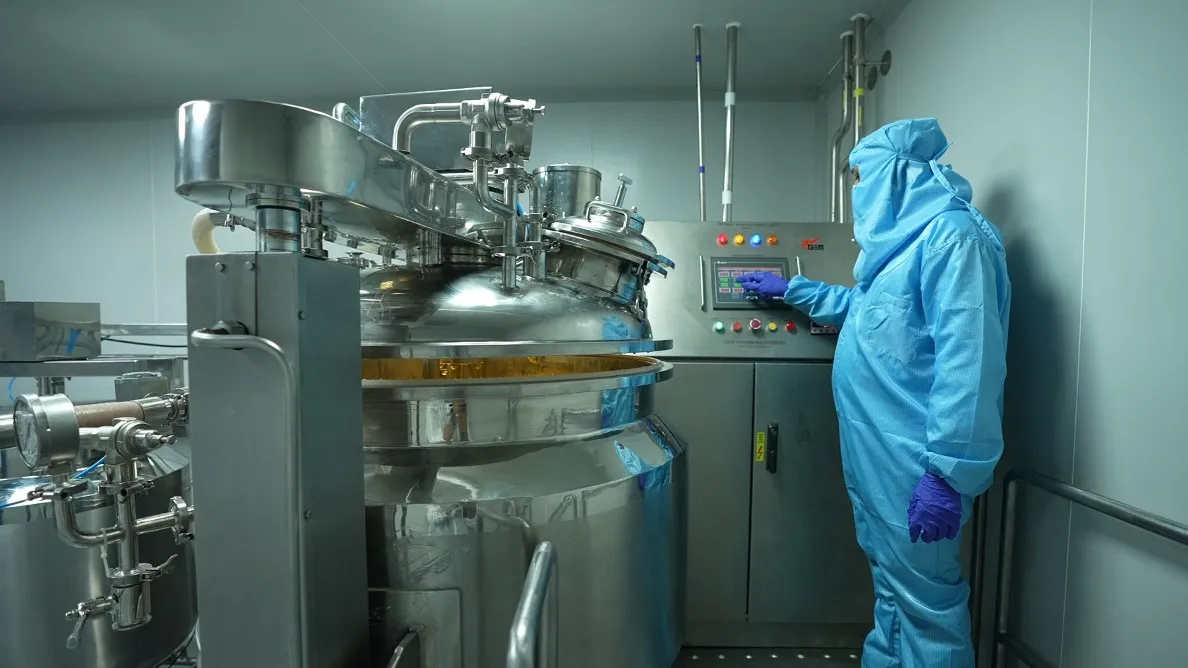
Ointment manufacturing vessel
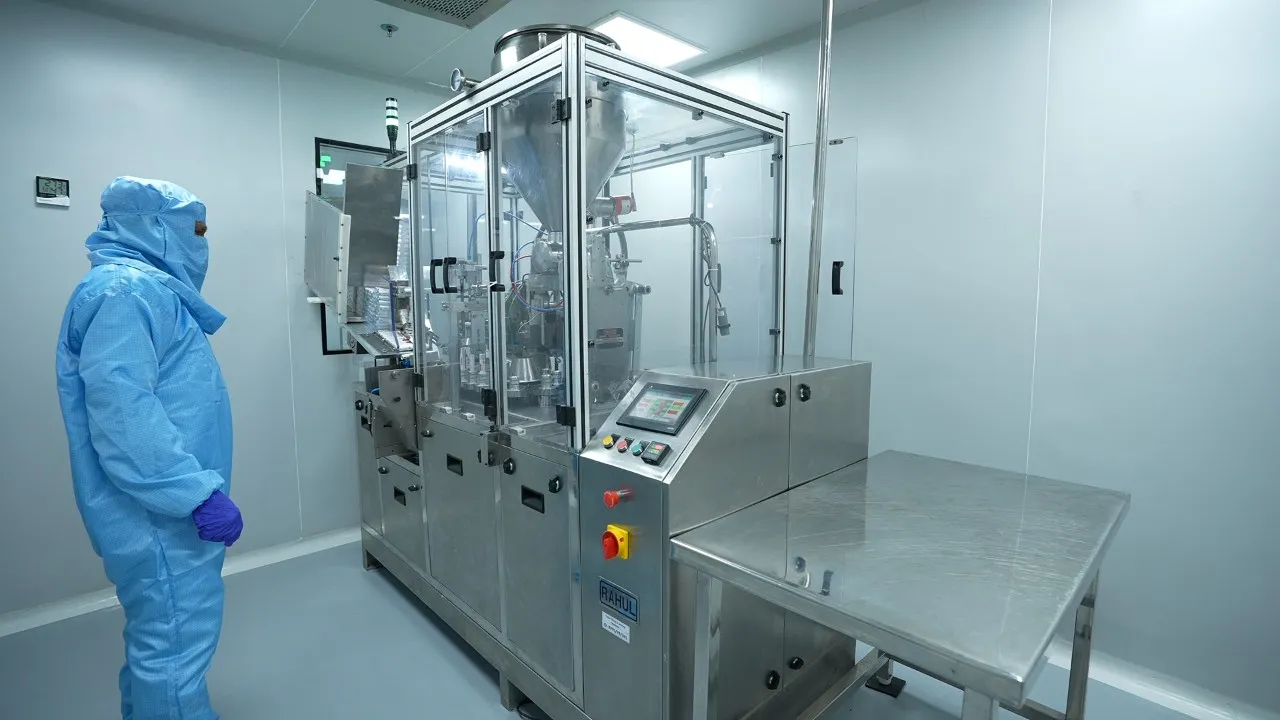
Tube filling machine
01 · Externals · manufacturing

Creams, ointments, gels, lotions.

Jacketed manufacturing vessels in a separate externals block.

02 · Externals · filling

60 million units a year.

Automatic tube filling and sealing, ready for cartoning and dispatch.

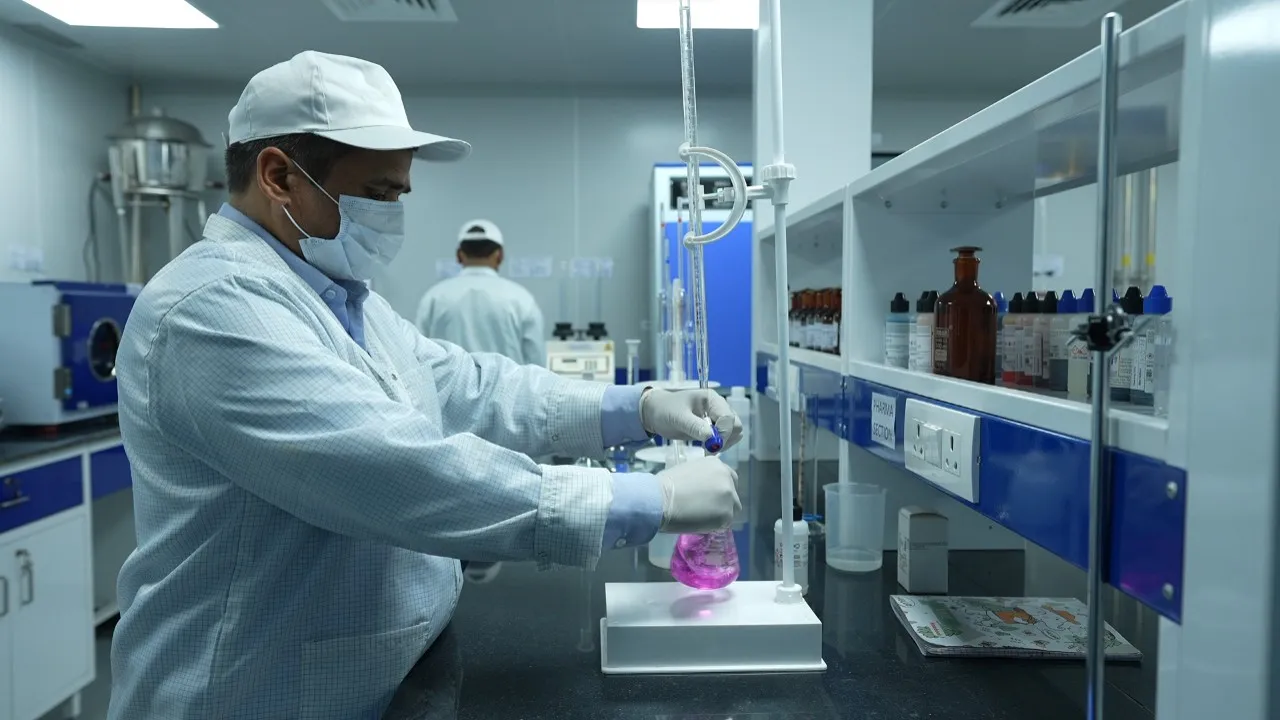
Scientist at work in the laboratory
Research and development

From formula to scale-up, under one roof.

Formulation development, process optimisation and technology upgrades by our in-house R&D team.